Material Cost and Utilization for Sheet Plastic
This section covers the following topics:
Material Cost
The cost of the material for a single part is given by the following formula:
Material Cost = (Part Volume * Cost Per Volume) / Utilization) / Final Yield
Material Cost depends on the following:
Part Volume
This is the volume of a single part after all operations are complete, obtained by GCD extraction and visible in the Geometric Cost Drivers panel.
Cost Per Volume
This is the cost of the part material per unit volume. aPriori calculates this as the product of the material properties Density and Unit Cost.
Utilization
This is the fraction of the mass of the workpiece’s raw material that remains after all operations are complete. The calculated value is a function of the selected Material Utilization mode in the Material Selection window:
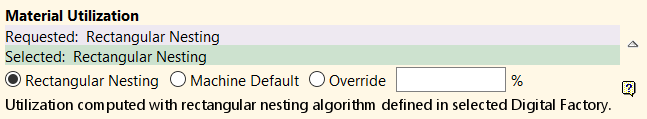
The options are as follows:
-
Rectangular Nesting: Utilization is equal to 1 - Waste. Waste is either Percent Scrap Per Sheet, or 0, whichever is greater. Percent Scrap Per Sheet is the percentage of scrap material created by the process. aPriori calculates Percent Scrap Per Sheet as Scrap Volume Per Sheet divided by Stock Volume:
-
Scrap Volume Per Sheet: the volume of sheet material that becomes scrap that may potentially be reground. See formula below.
-
Stock Volume: the product of stock Length, Width, and Thickness.
-
-
Machine Default: Utilization is equal to the machine property Avg Utilization.
-
Override: Utilization is equal to the Override value entered by the user.
Scrap Volume Per Sheet = Stock Volume - (Number Of Parts Per Sheet * Preformed Part Volume) + (Number Of Parts Per Sheet * Total Formed Hole Volume)
Scrap Volume Per Sheet depends on the following:
-
Stock Volume is as described above.
-
Number Of Parts Per Sheet is specified by the setup option Number of Parts per Sheet. Note that other setup options affect part nesting, including Minimum Sheet Length, Minimum Sheet Width, and Sheet Thickness. You can use the Material Nesting Review feature available on the Analysis Tool menu in the Component Viewer to view the effects of changes to these setup options on part nesting. For details, see Number of Parts per Sheet.
-
Preformed Part Volume is the product of Stock Thickness and the Parting Line Solid Shadow Area (the area of the outermost contour of the parting line’s projected shadow). Visible in the Geometric Cost Drivers panel.
-
Total Formed Hole Volume is the sum of all Simple Hole and Multistep Hole volumes from all operations in the routing. This represents the waste material from router cutting all Simple Holes and Multistep Holes in the part.
Final Yield
Final Yield is the fraction of parts created by this process in the current production scenario that will survive as good parts once any secondary processes are completed. That is, final yield is the fraction of parts created by this process that are not discarded as scrap parts, either by this process or by a downstream process. Final Yield is given by the following formula:
Final Yield = Output Volume / Input Volume
Final Yield depends on the following:
-
Output Volume: (Total Production Volume) the number of parts created by this process that are not discarded as scrap parts, either by this process or by a downstream process. It is the product of the annual volume and number of production years, specified in the Production Scenario screen of the Cost Guide.
-
Input Volume = the total number of parts produced by this process, including all parts discarded as scrap from this process or downstream processes. See formula below.
Input Volume = Output Volume + Lifetime Scrap Parts + Number of Scrap Parts Downstream
Input volume is the total number of parts produced by this process in the current scenario, including all parts discarded as scrap from this process or downstream processes. It is the sum of the following:
-
Output Volume: as described above.
-
Lifetime Scrap Parts: the number of parts discarded as scrap during this process. Scrapped parts include damaged, broken, or out-of-tolerance parts. See formula below.
-
Number of Scrap Parts Downstream: the number of parts discarded as scrap by downstream processes (if any).
Lifetime Scrap Parts = ((Output Volume + Number of Scrap Parts Downstream) / Good Part Yield) - (Output Volume + Number of Scrap Parts Downstream)
-
Output Volume: as described above.
-
Number of Scrap Parts Downstream: as described above.
-
Good Part Yield: the fraction of parts produced by this process that are not discarded as scrap by this process but may be discarded as scrap by downstream processes. By default, this is specified by the machine property Good Part Yield.